Skip to content

5- Axis CNC Machining

Simultaneous 5-axis milling on five vertical machining centers in Wauseon, Ohio, compound angles, angled holes and multi-sided parts finished in one setup.

 Steelcrest Precision runs 5-axis CNC machining for components that would otherwise need three or four setups on a 3-axis mill: impeller-style geometry, compound-angle ports, tilted holes and parts with features on five faces. Fewer setups means fewer datum shifts, tighter feature-to-feature relationships and shorter lead time. Located west of Toledo, we serve OEMs across northwest Ohio and nationwide, prototype through production.

steelcrest-brochure 1
Case Study: The Power of a Prototype-to-Production Process

Equipment & Capacity

Five-axis work at Steelcrest runs on two platforms: dedicated 5-axis vertical mills for prismatic and contoured parts, and INTEGREX multi-tasking centers where a part needs 5-axis milling and turning in the same cycle. The right platform depends on geometry, quantity and which features carry the tolerance. 
mill-5-axis-1200x675

SIMULTANEOUS 5-AXIS VERTICAL MILLING

  • 5 CNC 5-axis vertical mills, including a Haas UMC-750
  • Fleet capacity up to X=30", Y=20", Z=20"
  • True simultaneous 5-axis machining
  • Ideal for compound angles, angled holes, and multi-sided machining in fewer setups
mill-multi-tasking-1200x675

5-AXIS MULTI-TASKING (MILL-TURN)

  • INTEGREX and Hyper Quadrex platforms combine 5-axis milling, turning, and drilling in one setup.
  • Holding tolerances to ±0.0005" on milled features
  • Automated spindle-to-spindle transfer supports unattended machining
  • Max turning diameter / capacity
integrex-parts-1200x675

WHEN 5-AXIS IS THE RIGHT CALL

  • Features on three or more faces that must hold a positional relationship to each other
  • Angled holes, ports, or surfaces that would need a sine plate or custom fixture on a 3-axis machine
  • Contoured or organic surfaces where tool-axis control determines finish
  • Not automatically the answer — a simple part with one angled hole is usually cheaper on a 3-axis mill with a fixture. We quote the lower-cost route.

Tolerances and Surface Finishes We Hold

 Final tolerances depend on material, geometry, feature size and how the part is held. The figures below are what we hold as standard on 5-axis work; tighter callouts are reviewed at quote. 

Capability General Specification
Largest 5-axis part Up to X=30", Y=20", Z=20"
Side-milled surface finish Finishes up to 32 Ra
Face-milled surface finish  Finishes up to 63 Ra
5-axis CNC milling Holding tolerances to ±0.001″ 
Tilted-hole positioning Positional tolerances to ±0.003″ 
5-axis rotational positioning  Holding tolerances   to ±0.002″ –±0.003″ 
INTEGREX multi-task milling Holding tolerances to ±0.0005″ 
INTEGREX milled surface finish  Finishes up to 32 Ra 


5-Axis Parts We've Machined

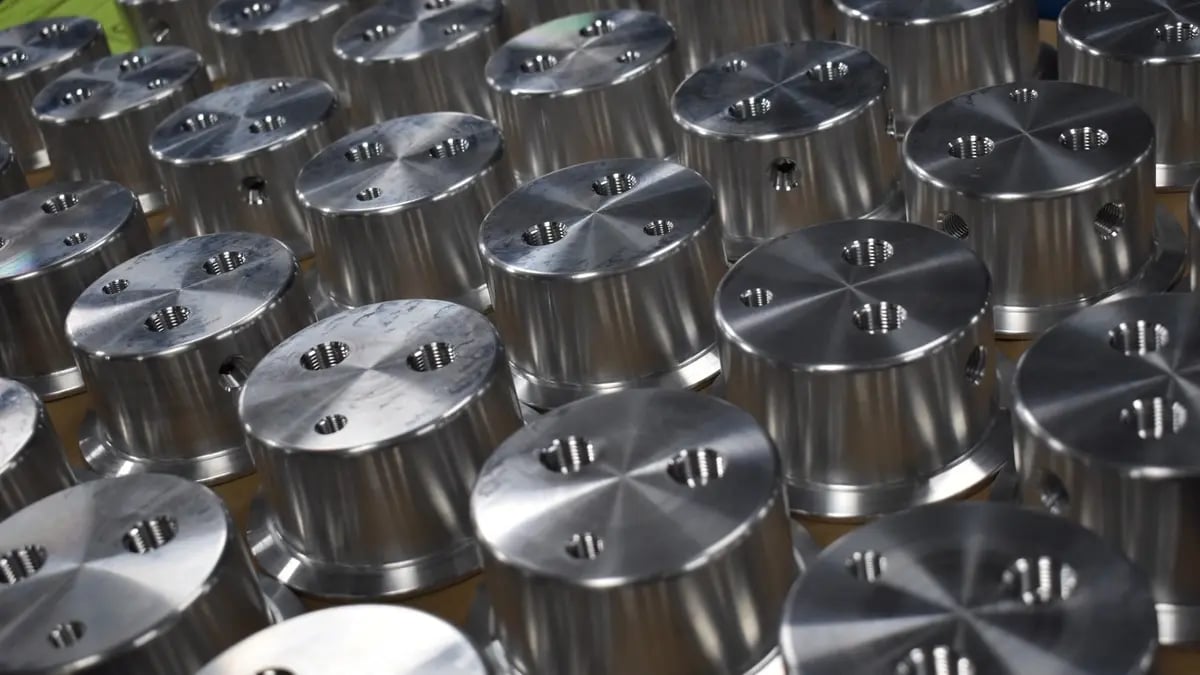
 Multi-face manifolds, compound-angle drilled caps, radial-port housings and contoured covers — each finished in one setup on our 5-axis mills in Wauseon, Ohio. 

Talk to a Machining Expert.

Share your drawing, material, tolerances, and production requirements. We'll help identify the right process for your program. 

Frequently Asked Questions

What 5-axis CNC machining services does Steelcrest Precision offer?

Steelcrest operates five CNC 5-axis vertical mills, including a Haas UMC-750, with fleet capacity up to X = 30 inches, Y = 20 inches, and Z = 20 inches, plus INTEGREX multi-tasking centers that combine 5-axis milling and turning in one setup. Work runs from prototype through production at our Wauseon, Ohio facility, west of Toledo. 

Do you run true simultaneous 5-axis or 3+2 positional machining?

True simultaneous 5-axis. All five axes move together during the cut, which is what allows contoured surfaces, compound angles and multi-sided features to be finished in one setup with continuous tool-axis control. 

When should a part be machined on 5-axis instead of 3-axis?

When features on three or more faces must hold a positional relationship, when angled holes or ports would need custom fixtures on a 3-axis machine, or when contoured surfaces need tool-axis control for finish. A simple part with one angled feature is usually cheaper on a 3-axis mill with a fixture — we quote the lower-cost route.

What tolerances can Steelcrest hold on 5-axis machining?

±0.001 inch on 5-axis milled features, ±0.003 inch positional on tilted holes, ±0.002 to ±0.003 inch on 5-axis rotational positioning, and ±0.0005 inch on INTEGREX multi-task milled features. Tighter callouts are reviewed at quote. 

What is the largest part you can machine on 5-axis?

Our 5-axis fleet handles parts up to X = 30 inches, Y = 20 inches, and Z = 20 inches. Larger multi-sided parts can run on our horizontal machining centers (X = 64 inches, Y = 50 inches, Z = 32 inches) with multiple setups. 

Does Steelcrest offer 5-axis multi-tasking (mill-turn) machining?

Yes. INTEGREX and Hyper Quadrex multi-tasking centers combine 5-axis milling, turning, and drilling in one setup, holding ±0.0005 inch on milled features. Automated spindle-to-spindle transfer supports unattended machining on production runs. 

Is 5-axis machining more expensive than 3-axis?

Per hour, yes. Per part, often not: one setup replaces three or four, which removes fixture cost, setup time and the datum-shift risk between operations. On multi-face parts the total is usually lower on 5-axis; on simple parts it is not. We quote both when the answer is not obvious.

Can you 5-axis machine titanium, Inconel, and stainless?

Yes. See our titanium, Inconel & nickel alloy, and stainless steel material pages for grades, tolerances and process notes. Difficult-to-machine alloys benefit from 5-axis because shorter tools and better approach angles reduce deflection and tool wear.

Do I need a 3D CAD model for a 5-axis quote?

A 3D model is strongly preferred. Five-axis toolpaths are programmed directly from the model, so a STEP or native CAD file with the drawing gives you a faster, more accurate quote and a shorter path to first article. If a model does not exist for a legacy part, tell us at RFQ. 

What information is needed to request a 5-axis machining quote?

A part drawing or 3D model, material specification, required tolerances, estimated quantities, surface-finish requirements, and desired delivery date. Include any inspection, heat treatment or finishing callouts. We respond within 48 hours.