Skip to content

Inconel & Nickel Alloy Machining Services

INCONEL & NICKEL ALLOY MACHINING SERVICES 

CNC Inconel and Nickel Alloy Machining for Extreme Heat and Corrosion 

Inconel does not behave like other metals, and the reason shows up on the invoice. These alloys work-harden the instant a tool stops cutting the cutting pressure itself creates the hardening. Let a drill spin at the bottom of a hole without feeding and the next tool will skate across a surface it cannot cut. Typical turning speeds run an order of magnitude below steel. None of that is a shop's inefficiency; it is what the material is. 

Steelcrest Precision machines Inconel 600, 625, 718 and X-750, along with commercially pure Nickel 200 and 201. We are ISO 9001 certified and machine to AS9100-compliant processes as we pursue full AS9100 certification. Turning holds ±0.0005", precision turning ±0.0002", and wire EDM ±0.0002" to ±0.0005", which on these alloys is often the right process rather than the fallback.  

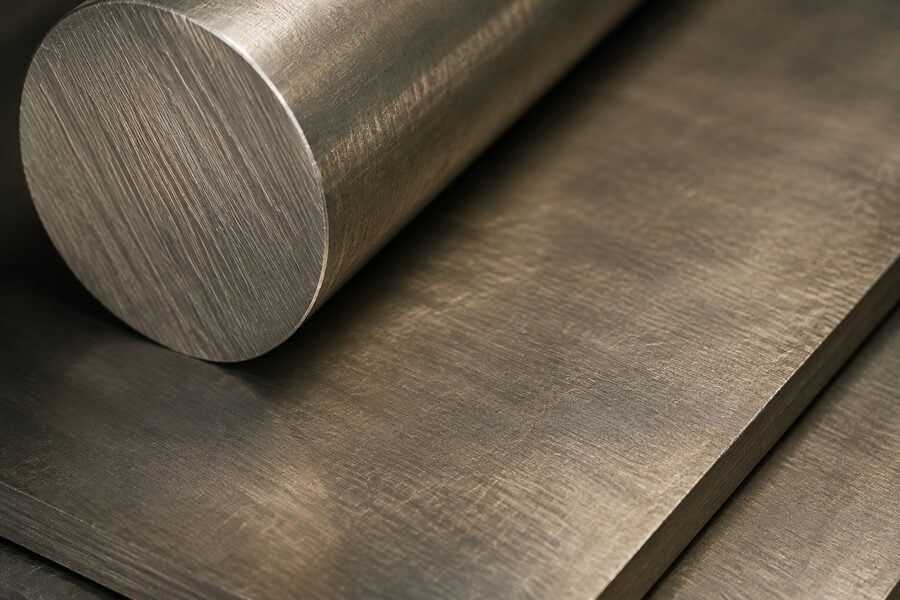
11-inconel-nickel-superalloys-texture

Nickel Alloys We Run

Alloy Type Typical use
Inconel 600 Solid solution Ni-Cr-Fe High-temperature and corrosion service parts. Behaves broadly like an austenitic stainless in the cut.
Inconel 625 Solid solution Ni-Cr-Mo Exhaust, ducting and corrosion-critical components. The gummiest of the four to get a good finish on.
Inconel 718 Age hardenable The aerospace workhorse high temperature structural and rotating components. Machined solution treated then aged, or machined aged where dimensions are critical.
Inconel X-750 Age hardenable Springs, fasteners and high temperature hardware.
Nickel 200 / 201 Commercially pure nickel Chemical and process handling components. 201 is the low-carbon version for service above 600°F.

Tolerances and Surface Finishes We Hold 

Our machine capability applies. What differs on nickel alloys is dimensional drift within a run tool wear, not machine capability, is what moves the size. We plan inspection frequency and insert change intervals around that rather than hoping for the best. 

Process Tolerance Surface Finish
CNC turning, standard ±0.0005" Up to 8 Ra
Precision turning ±0.0002" Up to 8 Ra, polishing available
CNC milling, 3- and 4-axis ±0.001" (excluding true-position callouts) 32 Ra side / 63 Ra face
5-axis milling ±0.001" linear · ±0.002–0.003" rotational · ±0.003" tilted-hole 32 Ra
INTEGREX / Hyper Quadrex mill-turn ±0.0005" 32 Ra
OD, surface and Blanchard grinding ±0.0005" to ±0.0002" Up to 8 Ra
Wire EDM ±0.0005" to ±0.0002" 16–32 Ra, fine to 8 Ra


NOTE*:  
On Inconel 718, machining after ageing holds size better than machining then ageing, because ageing causes dimensional change. Where the tolerance is tight, we buy aged bar at HRC 36–44 and machine to final size. Where the drawing calls for machine-then-age, we plan grind stock into the sequence. 

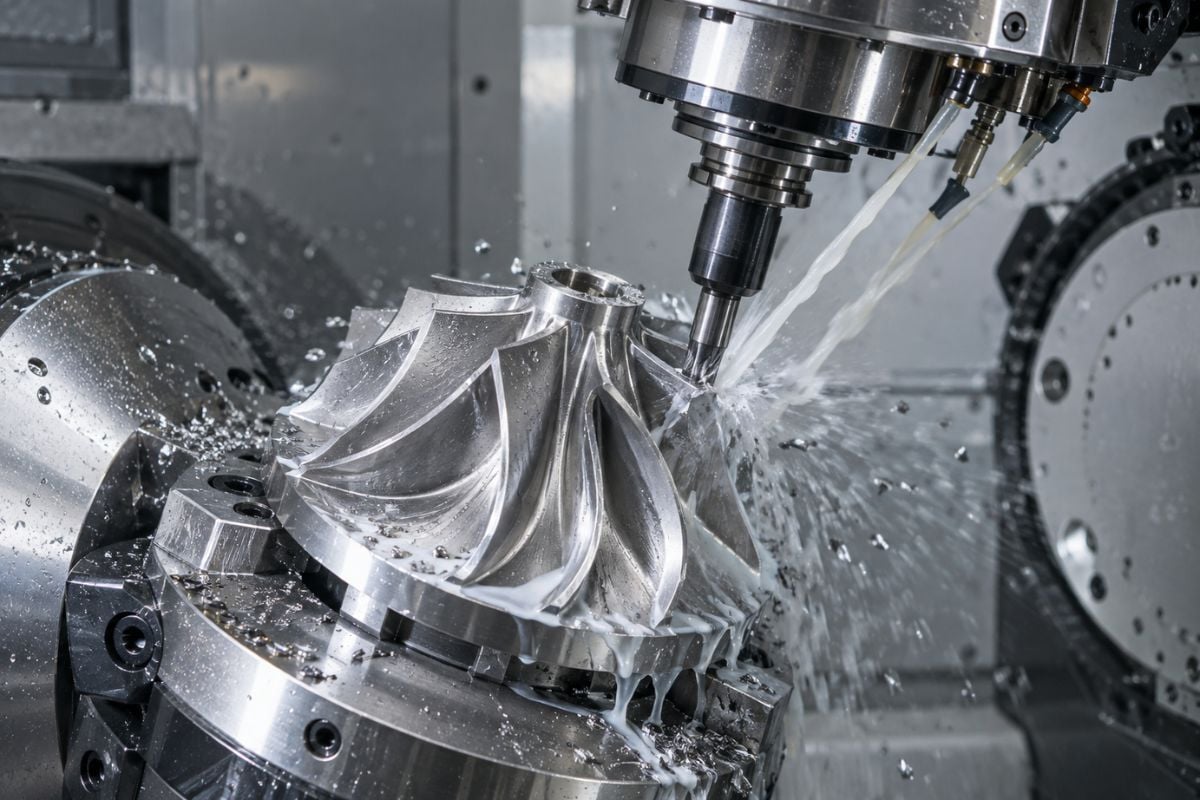
Five-axis CNC machining of a nickel-alloy aerospace component

How We Machine Nickel Alloys 

Milling runs across 36 vertical machining centers, eight horizontals at 64" × 50" × 32" and five 5-axis verticals the 5-axis platforms matter here because shorter, more rigid tool paths reduce the deflection and vibration that these alloys punish. 

Turning covers 28 CNC lathes to Ø26" × 160" with precision turning to ±0.0002", plus Swiss and bar fed platforms for smaller diameters and INTEGREX and Hyper Quadrex multi-tasking for one hit work. 

EDM is not a fallback on these materials, it is often the correct process. Five wire EDM machines at 31" × 28" × 11" and two RAM EDM machines at 24" × 14" × 10" cut features in Inconel that would take punishing tool life to mill slots, thin profiles, blind cavities and intricate geometry. OD grinding to Ø16" × 60" and surface grinding finish features tighter than turning will deliver. 

Why Inconel Costs What It Costs

Four material behaviors drive the cost of machining Inconel, and none of them can be engineered away. 


They work-harden as you cut them

Nickel alloys harden rapidly, and the high pressures generated during machining are themselves the cause. Practically that means constant feed with no dwelling, no rubbing and no spring passes; every pass has to take a real cut to get under the layer the previous pass created. Interrupt the process discipline once and you have a hardened surface and a dead tool. 

The heat has nowhere to go

Thermal conductivity is very low, so cutting heat goes into the tool and the workpiece rather than leaving in the chip. High pressure flood coolant is effectively mandatory, and even with it, tool life is a fraction of what the same geometry gives in steel. 

Notching at the depth-of-cut line

The characteristic failure mode is a notch worn into the insert exactly at the depth of cut. The counters are varying depth of cut between passes, using a lead angle, or ramping all of which add cycle time. 

Speeds an order of magnitude below steel

Typical carbide turning speeds on Inconel 718 sit around 100 to 200 surface feet per minute against many multiples of that in steel. Combined with insert life measured in minutes rather than hours, that is where the cost is. There is no supplier who has solved this the ones quoting substantially less are either not running the material or not running it correctly. 

There is no standardised machinability percentage for these alloys. The mill system groups them A through E: Inconel 600 sits in Group C, while 625, 718 and X-750 fall into Groups D-1 and D-2, the most difficult. Vendor figures of 10 to 15 percent circulate for 718 but are not from a primary source and we do not quote one. 

Nickel 200 and 201 

Commercially pure nickel is a different problem from the superalloys. It is the easiest of the nickel family and still difficult in absolute terms extremely gummy in the annealed and hot worked condition, work hardening rapidly, and producing long stringy continuous chips that make chip control a genuine production issue rather than a nuisance. 

The single highest-leverage decision on Nickel 200 and 201 is the stock condition: buy cold-drawn bar, not annealed. It changes the job more than any tooling choice will. Nickel 201 is the low-carbon version, specified for service above 600°F. 

Material certifications and a certificate of conformance ship with the parts, and we can hold mill certificates on file against your part number for repeat orders. 

08-nickel-alloy-steel-texture

Certification, Traceability and DFARS 

On aerospace nickel work, the documentation package is frequently the deciding factor rather than the machining. Steelcrest Precision is ISO 9001 certified, and we machine to AS9100-compliant processes as we pursue full AS9100 certification. We are also a member of the Precision Machined Products Association (PMPA). 

For defense contracts subject to the DFARS specialty metals clause, tell us at RFQ that your contract carries the clause. It determines where the material is bought and what documentation ships with the parts, and we confirm domestic-melt sourcing and the traceability chain, from mill certificate through finished part, before we quote. 

Material certifications and a certificate of conformance ship with the parts, and mill certificates can be held on file against your part number for repeat orders.
Finishing and Post-Processing

In-house at Steelcrest

  • Solution treatment and ageing within our 2100°F furnace range
  • Stress relief, saw cutting and bar preparation
  • Laser etching for lot traceability marking
  • Deburring, CMM and FARO Arm inspection

Managed through qualified partners

  • Descaling and pickling
  • Glass bead and grit blasting
  • Electropolishing well established for Inconel in semiconductor and pharmaceutical service
  • Shot peening on fatigue critical and rotating components


NOTE*:  
A specification detail worth knowing: ASTM A967 and AMS 2700 are stainless passivation specifications and do not cover nickel alloys. Commercial passivation of Inconel is offered but is not spec-governed specify the vendor process or your own customer specification rather than writing "passivate" on the drawing. 

Industries We Machine Nickel Alloys For

Steelcrest Precision machines Inconel 600, 625, 718 and X-750, along with Nickel 200 and 201, for aerospace and defense and medical and pharmaceutical applications. 

We also machine nickel superalloys for chemical processing, oil and gas and turbine customers who come to us directly. Those verticals do not have a dedicated page on this site, but they are a routine part of what runs through the shop. 

Talk To Us About Your Inconel & Nickel Superalloy Parts. 

Send the drawing and the quantity. We will come back with a real number, a real lead time, and if there is a better material or condition for what the part has to do we will tell you that too.

Frequently Asked Questions

Why is Inconel so much more expensive to machine than stainless?

Three reasons that compound. The alloys work-harden as they are cut, so every pass must take a real cut and process discipline cannot lapse. Thermal conductivity is very low, so heat goes into the tool rather than the chip and tool life is short. And typical turning speeds run around 100 to 200 surface feet per minute an order of magnitude below steel. The cost is in cycle time and tooling, and it is inherent to the material. 

Do you machine Inconel 718 before or after ageing?

Both, depending on the tolerance. Machining after ageing holds size better because ageing causes dimensional change, so where dimensions are critical we buy aged bar at HRC 36–44 and machine to final size. Where the drawing specifies machine-then-age, we plan grind stock into the sequence. 

Can you wire EDM Inconel?

Yes, and on many features it is the right process rather than a fallback. Five wire EDM machines at 31" × 28" × 11" hold ±0.0002" to ±0.0005" with no cutting force at all, which sidesteps both the work-hardening and the tool-life problem on slots, thin profiles and intricate geometry. 

Do you handle DFARS specialty metals requirements on nickel alloys?

Yes domestic-melt sourcing and full traceability from mill certificate to finished part on contracts carrying the clause. Raise it at RFQ. 

What is the difference between Inconel 625 and 718?

625 is solid-solution strengthened it cannot be age hardened, and it is the gummiest of the group to get a good surface finish on. 718 is age hardenable, reaching HRC 36–44, and is the aerospace structural and rotating-component workhorse. They are not interchangeable. 

Should I passivate Inconel parts?

If your customer specification calls for it, we manage it — but be aware that ASTM A967 and AMS 2700 are stainless specifications and do not cover nickel alloys. Specify the vendor process or your own specification rather than a generic "passivate" callout.