Steelcrest Precision
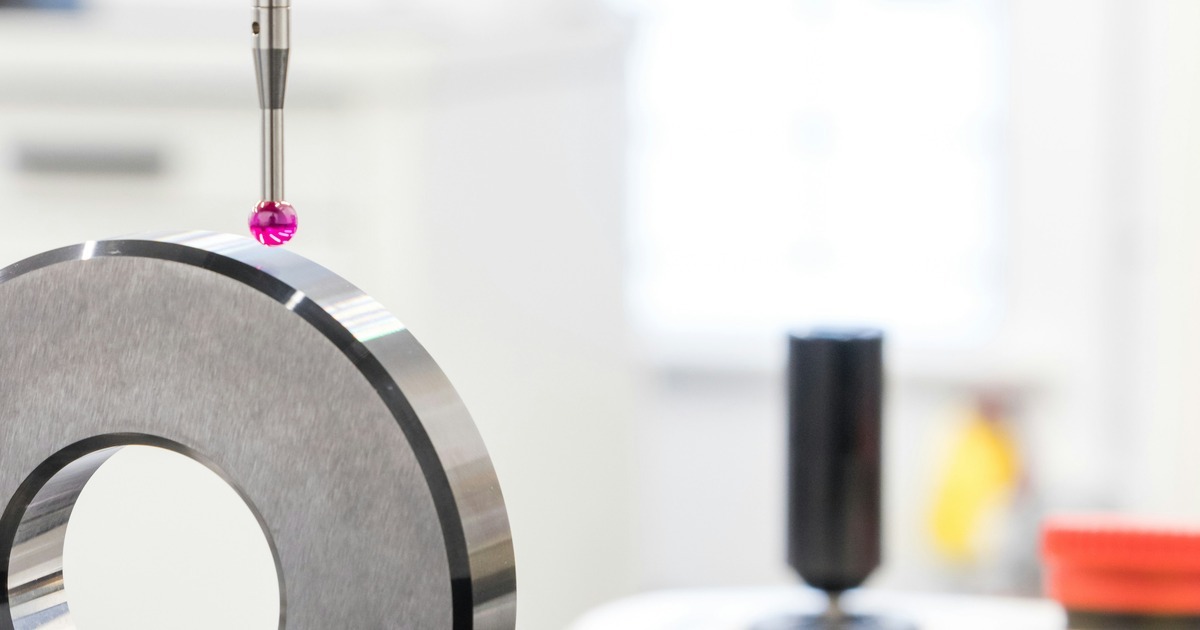

Most parts need less tolerance than their drawings specify. Industry-standard machining tolerance is about plus or minus 0.005 inch; precision work runs at plus or minus 0.001 inch; and only select features genuinely need the tighter bands grinding and honing provide. Set each tolerance from the feature's function, because every tighter decimal multiplies cost.
Every machine shop has seen the drawing: ±0.0005 inch on every dimension, including the ones that never touch another part. Somebody tightened everything to be safe, and the quote that came back was anything but. So instead of explaining tolerance in the abstract, let's follow one feature, a plain 1.000 inch bore, down the tolerance ladder and watch what happens to it. The processes behind each rung are covered in our complete guide to precision machining and on our capabilities page.
±0.005"
Standard
The bore comes off the mill or lathe finished. One setup, routine feeds, a calipers check on a sampling plan. This is the industry default band, and for a clearance hole it is all the bore will ever need.
±0.001"
Precision
Now the bore mates with something. Finishing passes, careful fixturing, a capable machine, and gauge or CMM verification. Industry cost studies put the part at roughly four times its rough-tolerance cost here. This band, the one the industry broadly calls tight, is Steelcrest's standard precision tolerance.
±0.0002"
High precision
The bore is now a bearing seat, and milling alone cannot hold it. The part earns a trip to grinding or honing, controlled conditions, and a per-feature inspection plan. At Steelcrest, select features are held here through our grinding, honing, and EDM departments, with tolerance capability tracked machine by machine so the work is routed to spindles proven to hold it.
Same bore, three different parts, three very different prices. The ladder is not a quality ranking. Each rung is the right answer for a different job, and the discipline is knowing which rung each feature of your part belongs on.
Notice what actually changed between rungs. The geometry never moved; the bore was 1.000 inch the whole way down. What changed was the process that makes it, the equipment that verifies it, and the risk the shop carries while doing both. That is why tolerance is the single strongest cost lever on a drawing: it is the one number that silently selects machines, operations, inspection methods, and scrap allowances all at once, before anyone talks price.
Because four things compound at once. The process changes: past a point, milling and turning hand off to grinding, honing, or EDM, and every added operation is a setup, a queue, and a schedule entry. Everything slows: finishing passes, reduced feeds, more frequent tool changes, sometimes temperature control. Inspection escalates: the calipers check becomes gauges, CMM time, and sometimes 100 percent inspection instead of sampling. And scrap risk gets priced in: a part that passes easily at ±0.005 can fail at ±0.001 even from a stable process. None of this argues against tight tolerances. It argues against unexamined ones.
One question does most of the work: what does this dimension touch? A surface that mates, locates, seals, or slides earns a tolerance derived from that fit. A surface that faces open air earns the standard band and nothing tighter. Three habits keep drawings honest:
Tolerance the fit, not the feature. A bearing bore needs its band because of the bearing, and the bearing manufacturer publishes exactly what that fit requires. Start from the mating component's specification, not from a house default.
Use the title block deliberately. A tight default in the title block silently applies to every undimensioned feature on the part. Set it at the standard band and call out the critical features individually.
Let the shop push back. A good machining partner reviews the drawing before quoting and flags the callouts driving cost without adding function. That conversation is free, and it is exactly the feedback our buyer's guide says to screen for.
Tolerance is a decision, not a default
Some features earn every dollar of their band. Bearing seats and press fits, where a thousandth of looseness becomes vibration and early failure. Sealing surfaces, where the finish and the dimension together decide whether the assembly leaks. Locating features on tooling and fixtures, where error multiplies into every part the tool ever makes. Gage work, where the part is the standard other parts get measured against.
In those places, precision is not gold plating. It is the function. The discipline is spending it there and nowhere else.
Three questions separate shops that hold tight work from shops that hope to. First: what is your standard tolerance, and what is your tightest, on which processes? The honest answer names different numbers for milling, turning, and grinding. Second: how do you know which machines can hold it? A professionalized shop tracks tolerance capability machine by machine and routes accordingly. Third: how will you prove it? Tight tolerance without matching inspection capability, calibrated gauges and CMM verification, is a promise with no receipt. A shop that answers all three in specifics is a shop you can hand your tightest drawing to.
Most machine shops treat about ±0.005 inch as the standard tolerance for metal parts, with plastics running looser at about ±0.010 inch. Steelcrest Precision works to a standard precision tolerance of ±0.001 inch, with tighter bands available through grinding, honing, and EDM when a feature requires them.
Tolerances tighter than roughly ±0.005 inch are generally considered tight in production machining, and bands at ±0.001 inch or below are firmly in precision territory. Below about ±0.0005 inch, work typically moves from milling and turning into grinding, honing, or EDM.
Substantially, and non-linearly. Industry cost studies show a part costing roughly twice as much at ±0.005 inch as at rough tolerance and roughly four times as much at ±0.001 inch, driven by added operations, slower cycles, heavier inspection, and higher scrap risk. Tolerancing only the features that need it keeps the curve working for you.
Routine CNC milling and turning reliably holds ±0.005 inch, and capable shops hold ±0.001 inch on functional features. Tighter than that, dedicated processes take over: precision grinding, honing, and EDM can hold select features to ±0.0002 inch with the right equipment, environment, and inspection.
Derive each tolerance from the feature's function: what it mates with, locates, seals, or slides against. Use the mating component's published fit requirements, set the title block default at the standard band, call out critical features individually, and ask your machine shop to review the drawing for callouts that add cost without adding function.
Send Us Your Tightest Drawing
A quote in 24 to 48 hours, and if we see tolerance driving cost without doing work, we will say so before you spend it.
Request a Quote